Industrial Conveyor Systems & Material Handling
Industrial Conveyor Systems & Material Handling
Custom Conveyor Solutions Designed Around Your Operation
Advanced Equipment & Supply provides conveyor, lift table, turntable, and specialty material handling solutions designed to improve product flow, reduce manual handling, and integrate seamlessly with your operation. From standard conveyor systems to custom-engineered applications, we help you select the right solution for your facility and production requirements.
Conveyor Solutions Built for Your Application
Every material handling operation has different products, layouts, production requirements, and challenges. AES provides a wide range of industrial conveyor systems and material handling equipment designed to move products efficiently and reliably. From belt and roller conveyors to chain conveyors, specialty systems, lift tables, and turntables, we can help you develop a solution around your workflow. Our team considers product characteristics, load requirements, available space, throughput, and integration with existing equipment to help improve efficiency and keep production moving.
Common Conveyor Types
-
Belt Driven Live Roller Conveyors
Versatile conveyor systems for boxes, cases, drums, totes, pallets, and other products requiring powered transportation, accumulation, diverting, or merging.Chain Driven Live Roller Conveyors
Heavy-duty conveyors designed to move pallets, tires, drums, and other demanding loads where durable, positive product movement is required.Chain Conveyors
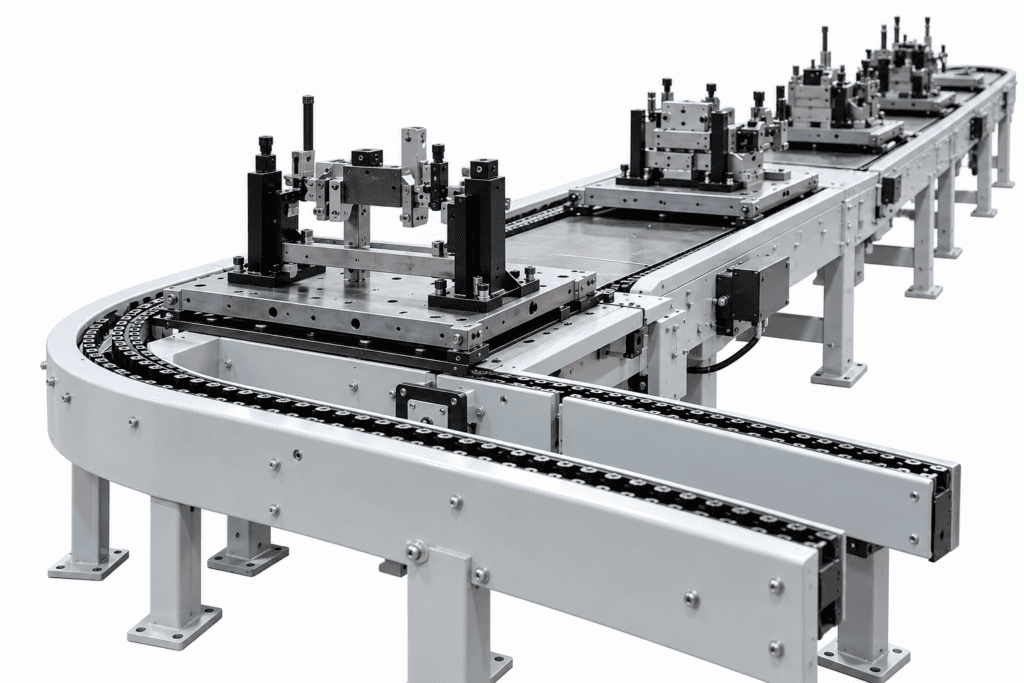
Ideal for products that are difficult to convey on rollers, including pallets, racks, automotive frames, and products with sturdy conveying surfaces.Belt Conveyors
Flexible conveyor systems for assembly, sorting, inspection, and transportation of products ranging from boxes and totes to bulky or irregular materials.Gravity Conveyors
Cost-effective conveyor solutions for warehouses, shipping areas, assembly lines, and other applications where products can move without powered assistance.Lineshaft Driven Live Roller Conveyors
Designed for lighter products and applications such as distribution, warehousing, food packaging, and parcel handling.Plastic Belt Conveyors
Low-maintenance, self-tracking conveyor systems with modular belts designed for reliable product movement and easy maintenance.Conveyor Rollers
A wide range of roller styles and sizes configured for standard applications or custom conveyor designs.Keep Your Operation Moving
Request a Quote Talk to a Conveyor SpecialistWhether you need a standard conveyor, specialty material handling system, lift table, or custom turntable, Advanced Equipment & Supply can help you develop a solution around your operation.
How to Choose the Right Conveyor
Choosing the right conveyor starts with understanding what you're moving and how it needs to move through your facility. AES evaluates your product, load requirements, production rate, available space, operating environment, and existing equipment to help identify the right conveyor system.
Key considerations include:
- Product Characteristics – Size, weight, shape, and handling requirements.
- Load Requirements – Individual product weight and overall conveyor capacity.
- Throughput – Required production rate and conveying speed.
- Facility Layout – Available space, elevation changes, turns, and transfers.
- Operating Environment – Temperature, moisture, chemicals, dust, and other conditions.
- System Integration – Compatibility with existing equipment, controls, and automation.
- Future Growth – Capacity and flexibility to accommodate changing production needs.
Custom & Specialty Conveyor Solutions
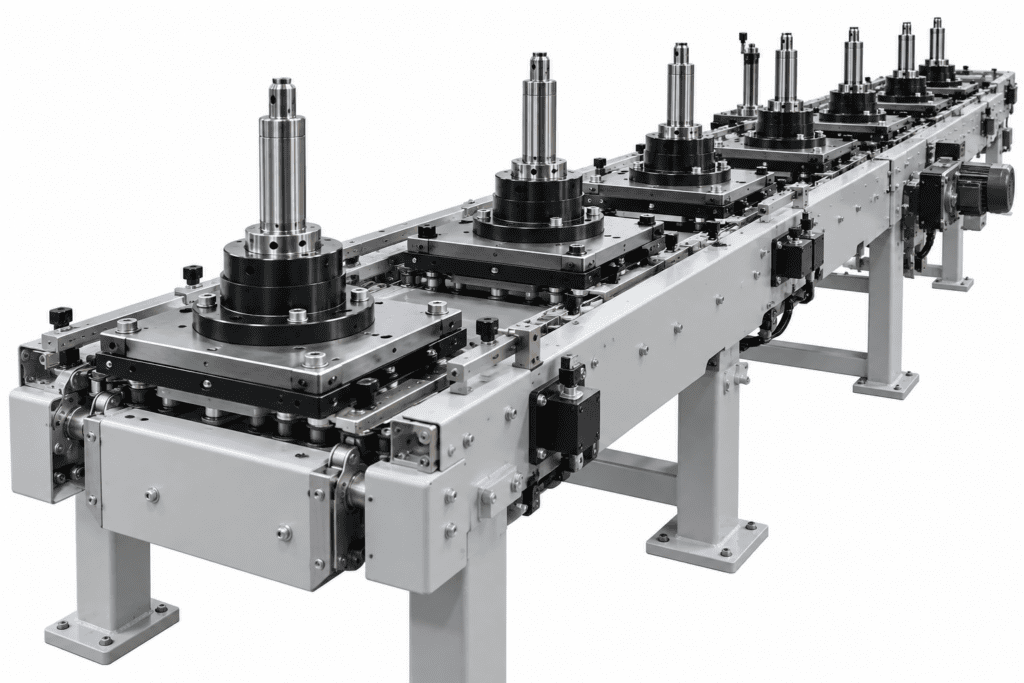
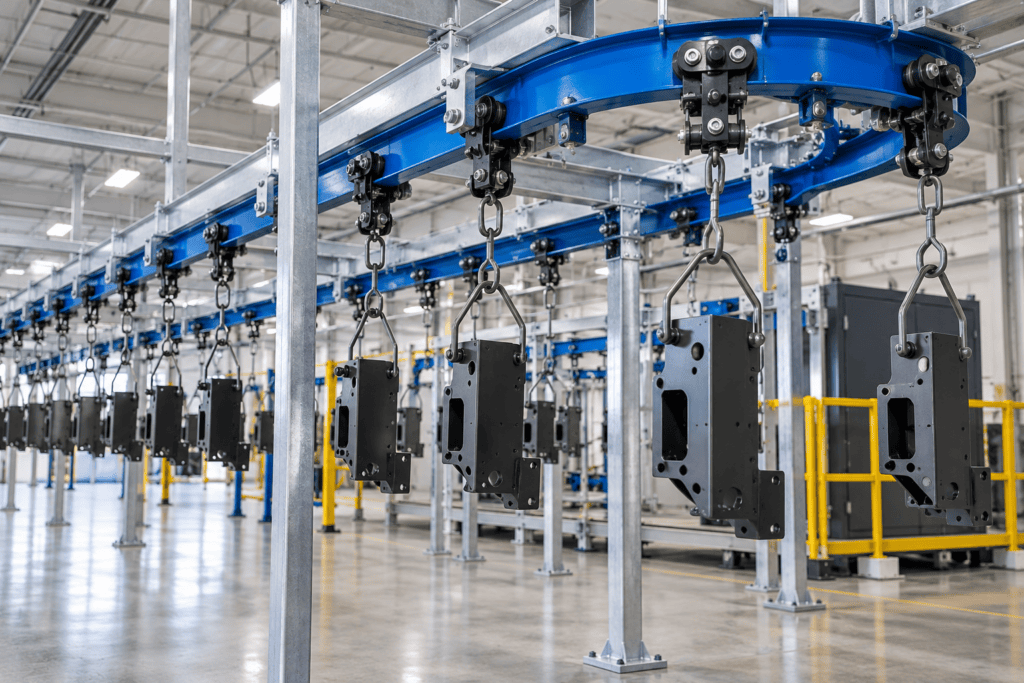
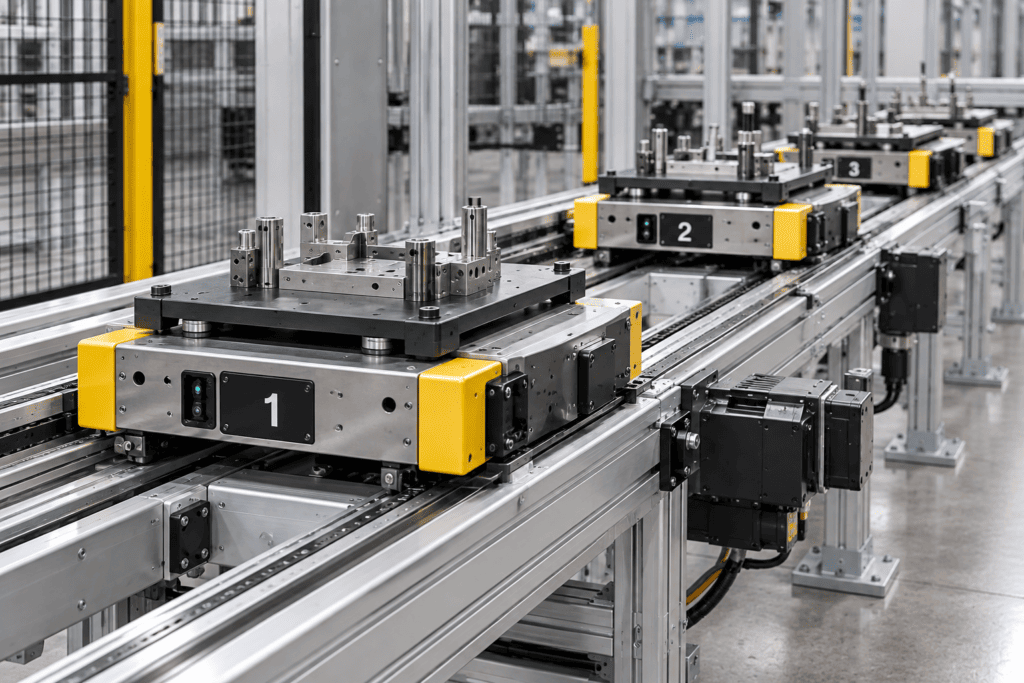
When a standard conveyor isn't enough, AES can develop a custom conveyor system around your operation. Our specialty solutions are designed for complex product handling, unique layouts, specialized positioning, and demanding production environments.
Lift Tables & Turntables
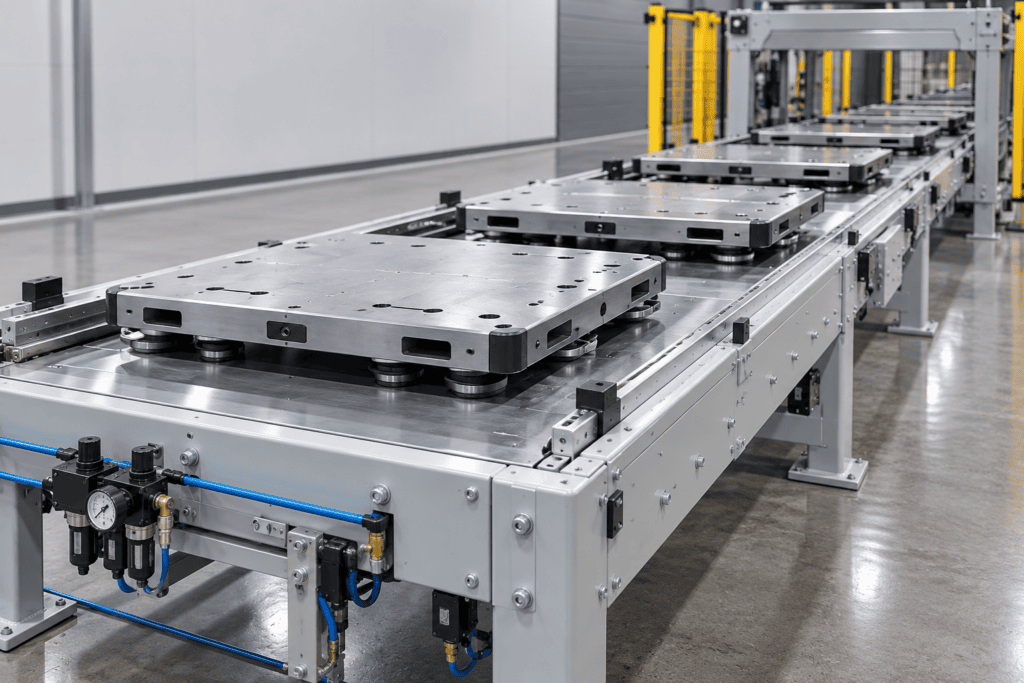
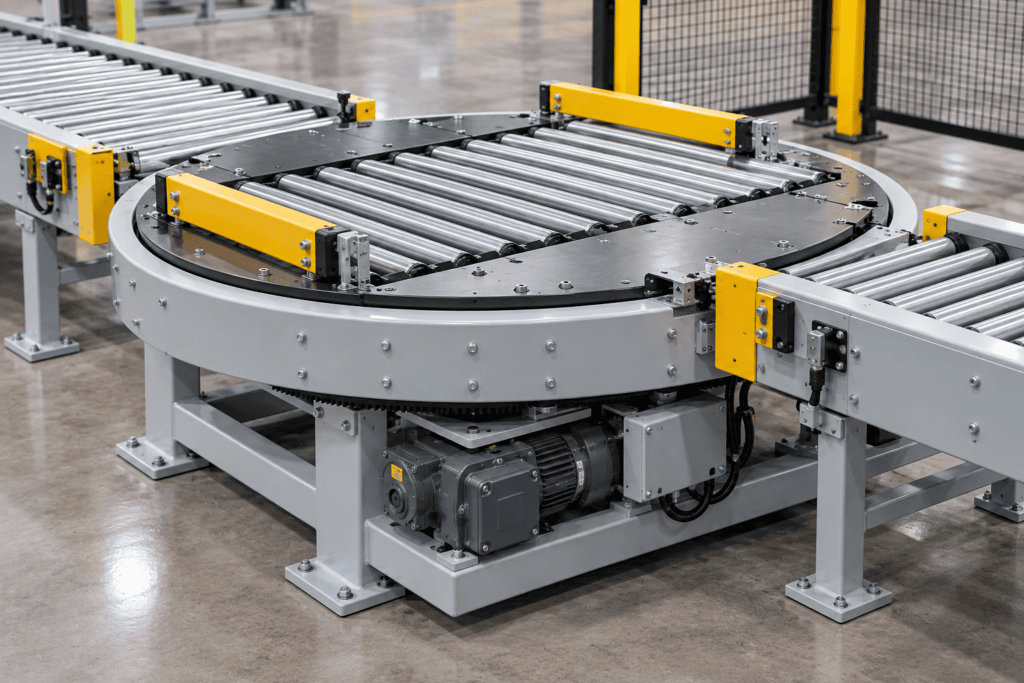
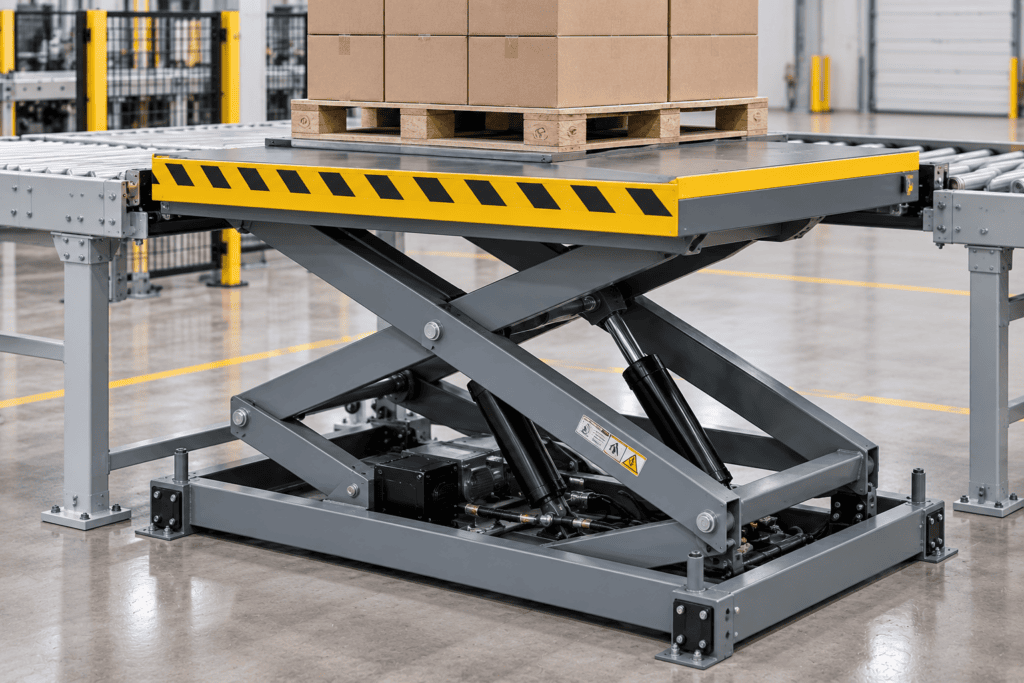
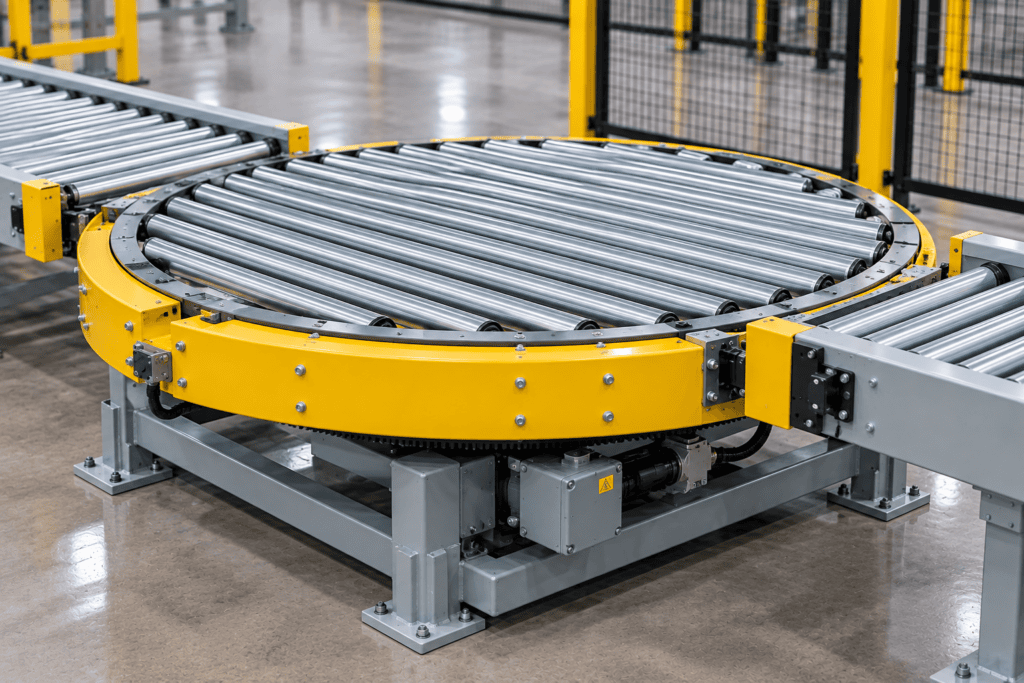
AES provides lift tables and turntables designed to improve material positioning, product transfer, and ergonomic access throughout manufacturing and industrial operations.
Ready to Find the Right Conveyor?
Material Handling Applications
Our conveyor and material handling solutions can be configured for a wide range of applications, including:
- Manufacturing & Assembly
- Warehousing & Distribution
- Agriculture & Grain Handling
- Food & Beverage
- Chemical Processing
- Packaging
- Material Transfer
- Product Sorting
- Product Accumulation
- Inspection & Assembly
- Pallet Handling
- Automated Production
Material Handling Solutions Backed by Experience
Request a Quote Talk to a Conveyor SpecialistAt Advanced Equipment & Supply, we take an application-focused approach to conveyor and material handling projects. We consider your products, production requirements, facility layout, and long-term goals to help identify equipment that improves efficiency and integrates with your operation.
Why Customers Choose AES
- Application-focused recommendations
- Standard and custom conveyor solutions
- Conveyor, lift table, and turntable options
- Specialty material handling expertise
- Integration with existing equipment
- Responsive technical support
Improve Efficiency with Custom Conveyor & Turntable Solutions
Whether you’re moving products through tight spaces, changing direction, or optimizing workflow, our team designs conveyor and turntable systems tailored to your operation. From standard equipment to fully custom solutions, we help you increase efficiency, reduce handling, and keep production moving.
Contact our team today to request a quote or speak with a Conveyor specialist.